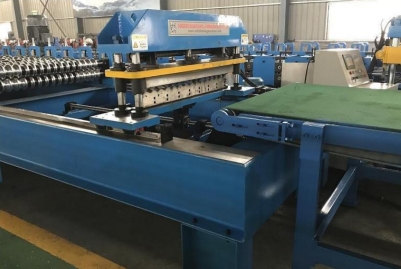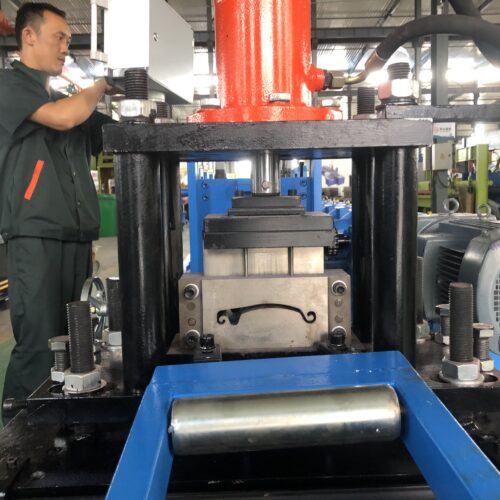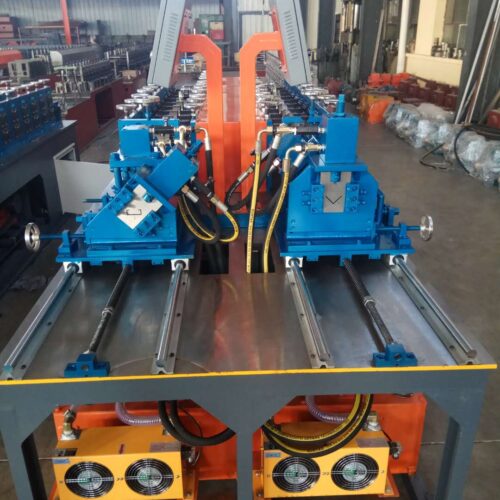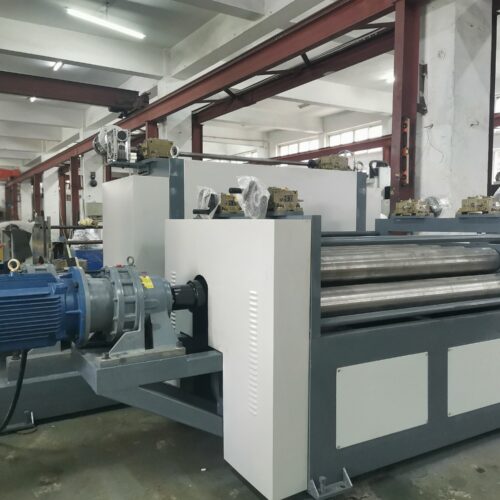
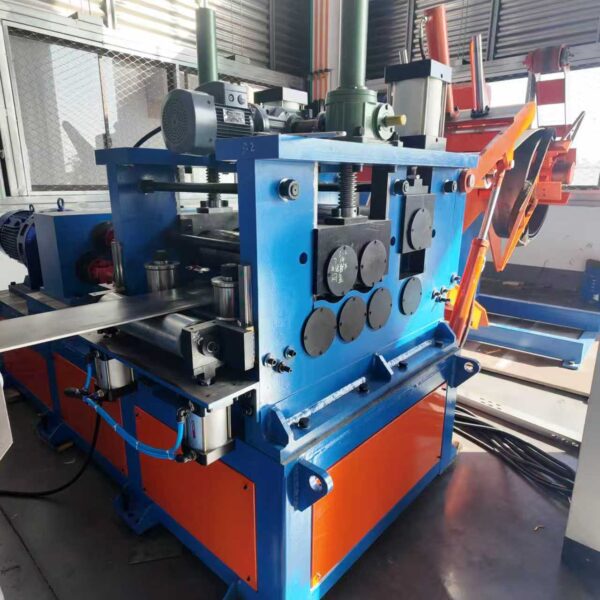
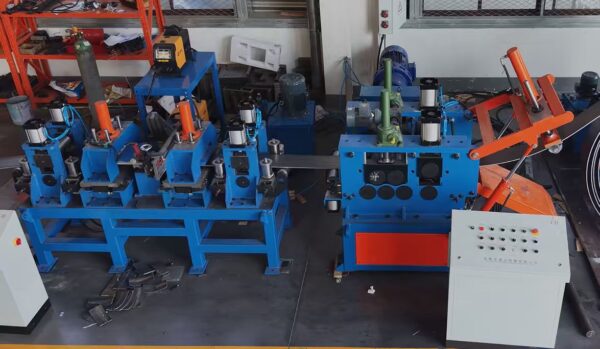
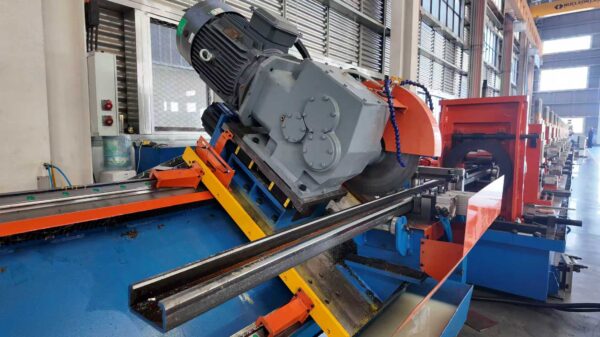


For HS800 truck frame rails, precision is not about one machine—it is about how five stages work together. This cold roll forming line turns 4.0–8.0 mm strip into 1–8 m profiles with PLC control, 16 forming passes, servo tracking cutting, and automatic stacking.
Line at a Glance
| Stage | Function | Key Specifications |
| Decoiling | Hydraulic automatic decoiling | 15 T; coil ID 610 mm; OD 1300–2000 mm; strip width 400 mm |
| Leveling | Five roll leveling and feeding | 30 kW AC variable speed drive; pneumatic guide rolls; hydraulic leveling rolls |
| Forming | 16 pass cold roll forming | 2 × 110 kW; 8–15 m/min; Cr12MoV rolls; 150 mm 42CrMo shafts |
| Cutting | Servo tracking hydraulic flying shear | 1–12 m; ±1 mm; 22 kW hydraulic station; 11 kW servo drag |
| Stacking | Intelligent unloading and stacking | 18 m roller conveyor; automatic stacking for 2.5–8 m rails |
Profile Range and Accuracy
| Item | Specification |
| Material | HS800 |
| Yield strength | 800 MPa |
| Strip thickness | 4.0–8.0 mm |
| Strip width | 400 mm |
| Bottom width | 186–250 mm |
| Web height | 60–70 mm |
| Corner radius | R12 |
| Flange angle | 90° ± 1° |
| Finished length | 1–8 m |
| Stacking length | 2.5–8 m |
| Straightness | ≤ ±1 mm / 6000 mm |
| Angle tolerance | ≤ ±0.5° / 6000 mm |
| Cut to length | ≤ ±2 mm / 6000 mm |
Why This Line Stands Out
| Feature | Benefit |
| 16 forming passes | Holds R12 corner and 90° flange in high strength steel |
| Servo tracking shear | Maintains ±1 mm cut accuracy while the line runs |
| PLC + HMI control | Manual/auto modes, fault monitoring, digital length setting |
| Automatic stacking | Reduces manual handling and keeps bundles aligned |
| Heavy duty forming host | Cast steel housings, 42CrMo shafts, Cr12MoV rolls for long service life |
Before Final Engineering
| Input | Why It Matters |
| Profile drawing | Defines roll design and pass schedule |
| Strip grade | Confirms HS800 or other high strength steel |
| Coil size | Matches decoiler and line layout |
| Target output | Sets line speed and automation level |
| Factory layout | Determines conveyor length and stacking position |
This cold roll forming line is built for stable, high-efficiency production of automotive frame rails. For final engineering, share the profile drawing, material grade, coil size, target output, and plant layout.